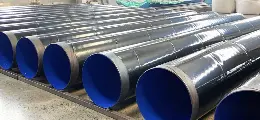
EN 10219 is the standard for cold-formed welded structural steel pipes developed by the European Committee for Standardization (CEN). It is widely used in construction, infrastructure, and industry. Longitudinal submerged arc welded (LSAW) steel pipes, a key product type under EN 10219, are the material of choice for long-distance oil and gas transportation, offshore engineering, and large-scale structural projects due to their excellent mechanical strength, dimensional accuracy, and pressure resistance.
EN 10219 Standard Overview
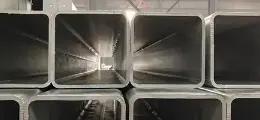
EN 10219 is a European standard for cold-formed welded structural hollow sections. It covers circular, square, rectangular, and elliptical shapes.
Material Grades: S235JRH, S275J0H, S355J2H
Wall Thickness: up to 40mm
Applications: bridges, buildings, offshore platforms
This standard ensures strict requirements for chemical composition, mechanical properties, dimensional tolerances, and testing methods.
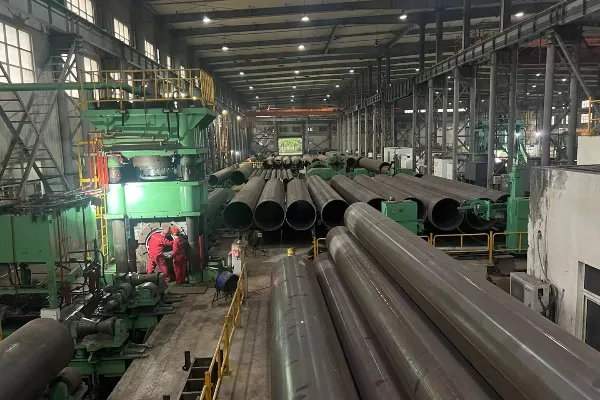
The manufacturing process for EN 10219 LSAW steel pipes combines high automation with strict quality control, involving multiple precision machining steps. Based on the forming method, LSAW steel pipes can be categorized into three main types: UOE, JCOE, and HME. Each type has its own unique characteristics during the forming stage, but the subsequent welding and inspection processes are largely the same. The UOE forming method uses dies to sequentially press steel sheets into U- and O-shapes, followed by diameter expansion (E), making it suitable for large-scale production. The JCOE method uses progressive stamping to form "J" and "C" shapes before closing them into an "O" shape, offering greater flexibility and enabling the production of thicker-walled pipes. The HME method utilizes mandrel rolling technology.
The LSAW steel pipe manufacturing process begins with steel plate inspection. The raw materials must meet the chemical composition and mechanical property requirements specified in EN 10219. Common steel grades include S235JR, S275J0H, and S355J2H. After entering the production line, the steel plates undergo full ultrasonic testing (plate probing) to ensure they are free of internal defects. Next, the milling process uses a dedicated milling machine to double-sided mill the edges of the steel plates to achieve precise plate width and parallelism, and to form the desired groove shape in preparation for subsequent welding. Pre-bending is a key step in the production of high-quality LSAW steel pipe. Using a pre-bending machine, the steel plate edges are pre-bent to achieve the required curvature, preventing the occurrence of straight edges during subsequent forming.
Advantages of EN 10219 LSAW Structural Pipe
High strength for heavy-duty projects
Excellent dimensional accuracy with expansion process
Superior pressure resistance
Large diameter range from 219mm to 1625mm
Wall thickness from 6mm to 75mm
Lengths up to 48 meters
Comparison of Pipe Types
|
Feature
|
EN 10219 LSAW Pipe
|
ASTM A500 Pipe
|
ERW Pipe
|
Seamless Pipe
|
|
Process
|
Submerged arc weld
|
Cold-formed ERW
|
ERW
|
Hot rolled
|
|
Strength
|
High structural
|
Medium-high
|
Medium
|
Very high
|
|
Diameter Range
|
Large (up to 1625mm)
|
Medium (up to 600mm)
|
Small-medium
|
Limited
|
|
Pressure Resistance
|
Excellent
|
Good
|
Good
|
Excellent
|
|
Cost Efficiency
|
High for large size
|
Good
|
Very good
|
Expensive
|
Manufacturing Process of EN 10219 LSAW Pipe
1.The production of EN 10219 LSAW structural pipe is a highly controlled process that combines advanced machinery with strict quality assurance. Each step plays a crucial role in ensuring the pipe meets international standards.
2.Raw Material Inspection: Only steel plates that meet the chemical and mechanical requirements of EN 10219 are used. Plates undergo ultrasonic testing to ensure they are free from internal defects.
3.Edge Milling: Precision milling machines prepare the plate edges, ensuring smooth and uniform weld preparation with accurate bevel angles.
4.Pre-bending: The edges are pre-bent to reduce stress during forming. This avoids straight edges and ensures a smooth circular shape.
5.Forming: Using UOE or JCOE methods, plates are gradually shaped into cylindrical pipe blanks. UOE is ideal for large-scale production, while JCOE offers flexibility for thicker pipes.
6.Tack Welding: The seam is initially joined with protective welding, keeping the pipe stable for further processing.
7.Double-Sided Submerged Arc Welding: The inside and outside seams are welded separately. Multiple wire systems are often used to improve penetration and productivity.
8.Mechanical Expansion: After welding, the pipe is expanded to achieve precise roundness and reduce residual stress.
9.Testing: Non-destructive testing methods such as X-ray inspection, ultrasonic testing, and hydrostatic pressure testing verify that each pipe meets safety standards.
FAQs
What is EN 10219 LSAW structural pipe?
It is a longitudinally welded pipe manufactured under EN 10219 standards for use in structural and industrial applications.
How is EN 10219 different from ASTM A500?
EN 10219 is a European standard with stricter low-temperature and structural requirements, while ASTM A500 is mainly for U.S. construction applications.
What sizes are available for EN 10219 LSAW pipe?
Diameters range from 219mm to 1625mm, with wall thicknesses between 6mm and 75mm. Custom lengths up to 48 meters are possible.
Where is EN 10219 LSAW pipe used?
It is widely used in bridges, offshore projects, pipelines, foundations, and industrial frameworks.
 English
 Español
 بالعربية
 Phone :
 Whatsapp :
 Email :